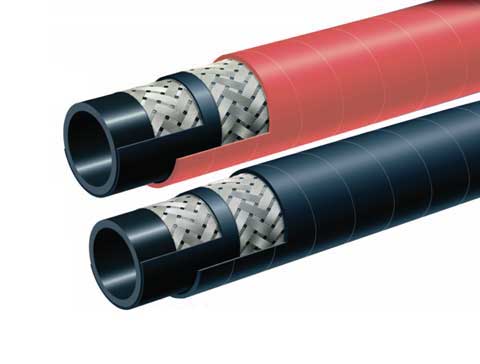
Steel-wire-spiral-reinforced hydraulic hoses for mining use, compliant with the EN 856 standard and holding MA certification
release date:2026-11-09 10:09:40
reading volume:
share:
In the high-pressure hydraulic systems of fully mechanized coal mine working faces, the reliability of hydraulic hoses is a critical factor in the operational safety of support equipment. Standard industrial-grade hoses are neither capable of withstanding the rigorous underground operating conditions nor do they meet the mandatory compliance thresholds for coal mine safety certification. Steel-wire-reinforced hydraulic hoses that comply with the EN856 standard and hold the "MA" (Mining Product Safety) certification bridge the gap between advanced European performance standards and domestic mandatory safety requirements. By meeting stringent criteria—including pressure-bearing capacity, resistance to impulse fatigue, flame retardancy, and antistatic properties—these hoses serve as essential, high-performance, and fully compliant transmission components for high-pressure hydraulic systems in underground coal mines.
Full-spectrum alignment with the EN856 standard ensures long-term reliability under high-pressure, heavy-duty conditions.
 As an internationally recognized benchmark for high-pressure, steel-wire-reinforced hydraulic hoses, the EN856 standard imposes rigorous requirements—far exceeding those of typical industry standards—on key performance indicators such as pressure stability, impulse fatigue life, and temperature adaptability. From material selection to the entire manufacturing process, these mining-specific hydraulic hoses are engineered to align with the technical requirements of the EN856 standard. This allows them to significantly surpass the performance limits of conventional mining hoses, delivering an exceptionally long service life even under high-pressure, heavy-duty operating conditions.
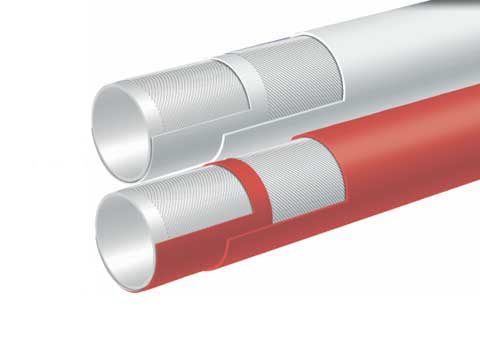
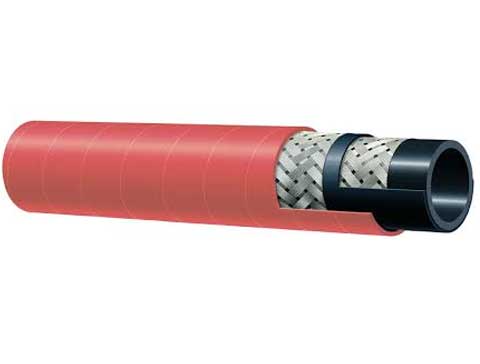
The inner rubber layer of the hose strictly adheres to the oil-resistant synthetic rubber specifications mandated by the EN856 standard. It remains resistant to swelling and degradation even during prolonged exposure to anti-wear hydraulic fluids used in mining, across a wide temperature range of -40°C to 100°C. Furthermore, the material can withstand short-term temperature peaks of up to 125°C, making it perfectly suited for the thermal environment in which underground coal mine hydraulic systems operate continuously. The multi-layer, high-strength steel wire reinforcement utilizes a balanced-angle, bi-directional interlaced winding process as specified by the EN856 standard. The density and winding tension of each steel wire layer are precisely calibrated. Depending on the hose diameter, the working pressure ranges from 28 MPa to 45 MPa, with a burst pressure exceeding four times the rated working pressure. This provides a safety margin far greater than that of conventional mining hoses, effectively withstanding the transient high-pressure surges that occur during the startup/shutdown of underground hydraulic systems or the rapid movement of hydraulic supports.
Impulse fatigue testing, conducted in accordance with the EN856 standard, demonstrates that this hose’s service life under rated pressure significantly exceeds the minimum requirements—outperforming standard braided mining hydraulic hoses by several times. Even under the long-term stress of high-frequency pressure pulses common in underground operations, the hose remains free from premature steel wire breakage or internal blistering. Furthermore, its low-temperature flexibility fully complies with the EN856 standard; when bent to the specified minimum radius at an extreme temperature of -40°C, the hose wall shows no signs of cracking. This ensures consistent flexibility and structural integrity, even in the harsh, cold-climate, high-altitude underground environments of coal mines, with no risk of brittle fracture.
Full-material compliance with MA certification ensures intrinsic safety for high-risk underground environments.
Underground coal mines are high-risk environments prone to fire and explosion hazards. Consequently, all non-metallic piping components must obtain the "Mining Product Safety Mark" (MA certification) to be legally permitted for use underground. Every material used in this steel wire-reinforced hydraulic hose—from the inner liner to the outer cover—has been specifically developed to meet mining safety regulations. The product fully satisfies all mandatory technical requirements for MA certification, ensuring complete compliance from individual components to the final assembled unit. The outer rubber layer of the hose utilizes a specialized flame-retardant and anti-static compound designed for coal mine applications. It has undergone rigorous flame-retardancy testing: when exposed to an alcohol blowtorch flame, the outer rubber self-extinguishes almost immediately upon removal of the heat source, ensuring there is no risk of sustained combustion or the spread of flames along the hose assembly. Furthermore, the volume resistivity of the outer layer is strictly maintained within the anti-static range mandated by mining safety standards. This allows for the continuous and stable dissipation of static electricity generated during dragging or friction in underground operations, effectively eliminating the risk of static accumulation and discharge—a critical hazard that could otherwise ignite mine gas or coal dust.
The inner rubber layer and the intermediate isolation layer are constructed from oil-resistant, flame-retardant materials that meet "MA" (Mining Safety) certification requirements. In the event of extreme operating conditions—such as damage to the inner layer leading to high-pressure oil seepage—these non-metallic materials will not be dislodged by the pressurized oil and subsequently ignite upon contact with an open flame. All non-metallic components of the hose assembly have passed mandatory mining safety tests for flame retardancy, anti-static properties, and toxic gas emissions; they do not release harmful fumes during underground use, fully complying with the safety environment requirements for coal mines. The accompanying metal couplings have undergone anti-corrosion passivation treatment, ensuring they remain resistant to rapid rusting or degradation of mechanical properties, even in the high-humidity, corrosive environment typical of underground mines. The crimped connection between the coupling and the hose meets all tensile strength requirements stipulated by the MA certification, preventing the hose from detaching from the coupling under high-pressure conditions. The entire hose assembly has successfully passed comprehensive testing by a national mining product safety inspection authority and has been granted full MA certification. Consequently, coal mine operators can deploy these hoses underground immediately upon procurement, without the need for additional on-site verification. Dual-Standard Compliance for Comprehensive Mining Applications: Enhancing Safety and Efficiency Throughout the Lifecycle
By simultaneously meeting both the EN856 performance standard and the mandatory MA (Mining Product Safety) certification for underground mining, this hydraulic hose is ideally suited for virtually all high-pressure hydraulic applications in coal mines. It effectively resolves common industry pain points: standard mining hoses often lack sufficient performance, while high-end imported alternatives may meet performance requirements but fail to comply with regulatory standards. This solution delivers both safety and operational efficiency for coal mine operators throughout the entire product lifecycle.
In the main circuits of high-capacity hydraulic roof supports at fully mechanized longwall faces, the hose’s exceptional impulse resistance enables it to withstand 31.5 MPa high-pressure, heavy-duty operating conditions. Its service life far exceeds that of conventional mining hoses, significantly reducing the frequency of high-risk hose replacements in confined underground spaces and minimizing the time personnel must spend in hazardous zones at the working face. In the high-pressure hydraulic systems of underground tunneling equipment, the hose’s superior resistance to bending and deformation allows it to endure the constant movement and flexing that occur as a roadheader advances. This prevents premature hose bursts at bend points, ensuring the continuous, efficient progress of excavation operations. Furthermore, in the hydraulic drive circuits of large-scale equipment within underground main transport systems, the hose’s wide operating temperature range ensures stable, long-term performance without degradation, regardless of temperature variations across different mine areas.
For coal mining operations, adopting this steel-wire-reinforced hydraulic hose—which satisfies both EN856 standards and MA certification—offers significant advantages. Its extended service life drastically reduces the frequency of high-pressure hose replacements and lowers overall spare-part procurement costs. It also helps prevent unplanned production line stoppages caused by sudden hose bursts, thereby avoiding substantial losses in output. Moreover, full MA certification ensures complete compliance with coal mine safety regulations, eliminating the risks associated with using uncertified components underground and fundamentally removing major safety hazards—such as gas or coal dust explosions—that could otherwise be triggered by the failure of a high-pressure hydraulic hose. During routine operation and maintenance, regular inspections for external wear—conducted in accordance with coal mine safety regulations—along with periodic spot checks of anti-static properties, ensure long-term, stable performance. This establishes a robust, dual-layered defense—combining high performance with intrinsic safety—for high-pressure hydraulic systems used in underground coal mines.
As the intelligent transformation of coal mining continues to advance in China, the operating pressures and continuous run-times of underground high-pressure hydraulic systems are steadily increasing. Consequently, specialized hydraulic hoses that meet both advanced international performance standards and mandatory domestic safety requirements for mining equipment are becoming the preferred choice for high-end, modernized mines, providing a reliable foundation for fluid transmission that supports safe and efficient coal production.
Previous: